From forecast to shop floor, one plan the plant can actually run.
M-APS is Magellan's planning and scheduling platform. It connects demand forecasting, the master production plan, finite-capacity scheduling and shop-floor tracking in a single loop, and explains every recommendation before anyone approves it.
Planning and execution usually run on separate tracks.
The plan is built in one spreadsheet, the sequence in another, and the shop floor finds out what changed when the order is already late.
The plan ignores capacity
Monthly volumes are set against demand without checking machines, shifts, maintenance or setups. The gap shows up as overtime and missed dates.
The schedule is a black box
Sequences are produced or adjusted by hand, and nobody can say why order A runs before order B. Hard to trust, harder to change.
Errors travel downstream
A wrong forecast becomes a wrong plan, then a wrong sequence, then a late order. Without traceability, the cause is found weeks later.
One loop, from demand to the machine and back
Each step feeds the next, and what happens on the shop floor flows back into the plan. Every change is versioned, approved by a person and only then published.
Forecast
statistical demand forecast per SKU, with a confidence range
Master plan
volumes by month, lot sizing and rough-cut capacity by resource group
Scheduling
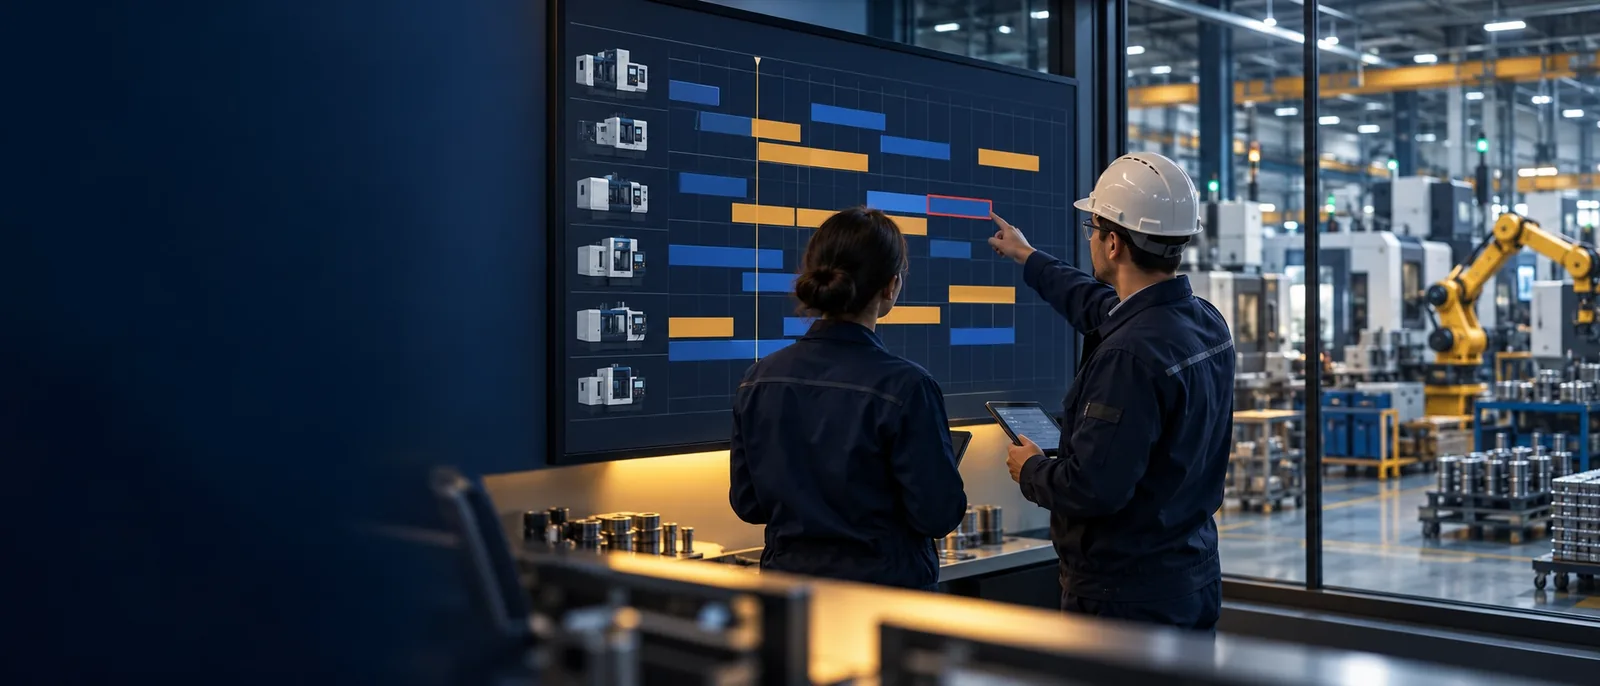
finite-capacity sequence of orders on machines, optimised
Shop floor
order status, planned vs. actual, operator events
Diagnosis
what went wrong, why, and a recommended action
Approval
a named person approves; nothing is applied automatically
The sequence is built on the constraints your planners already know.
Shifts and breaks, maintenance windows, setups that depend on what ran before, real machine efficiency (OEE), alternative routings and work already in process. When an order is at risk, the platform says which order, on which machine, why, and what to do about it.
Order 1047 will finish 2 h 40 min after its due time. Machine M03 is overloaded in shift 2: the maintenance window from 10:00 to 12:00 pushed orders 1046 and 1047 into the afternoon.
Recommendation: move order 1047 to its alternative routing on M04, which has free capacity after 14:30. Estimated effect: on time, with one extra setup.
Built for decisions people can defend.
Every recommendation explained
Forecasts break down into trend and seasonality. Each finding points to its cause, and each recommendation comes with its reasoning, traceable back to the data.
People decide
Plans are versioned, approved and published by a named user. Nothing is applied automatically, and every decision is recorded.
A closed loop
Shop-floor events return to scheduling, and stock is reconciled into the master plan at period close. A forecast risk can be traced to the orders it will affect.
Alerts with an owner
When something needs action, the alert goes to a responsible person with a deadline, by e-mail, push or andon, and stays open until it is handled.
Plants with many orders, many machines and real constraints.
Discrete and batch manufacturing, from machining to food and pharmaceuticals, where sequence changes cost and capacity is shared.
It starts with your data, not with the software.
Diagnostic
We assess the maturity of your planning data and define the scope of a first pilot.
Pilot
One plant or one area, running on real data, with your planners in the loop.
Scale
More areas and integration with your ERP and MES, at the pace the routine absorbs.
Where is planning costing you today?
Tell us about your plant: orders, machines, constraints and how the plan is built today. We will show where the loop breaks and what M-APS would change.